
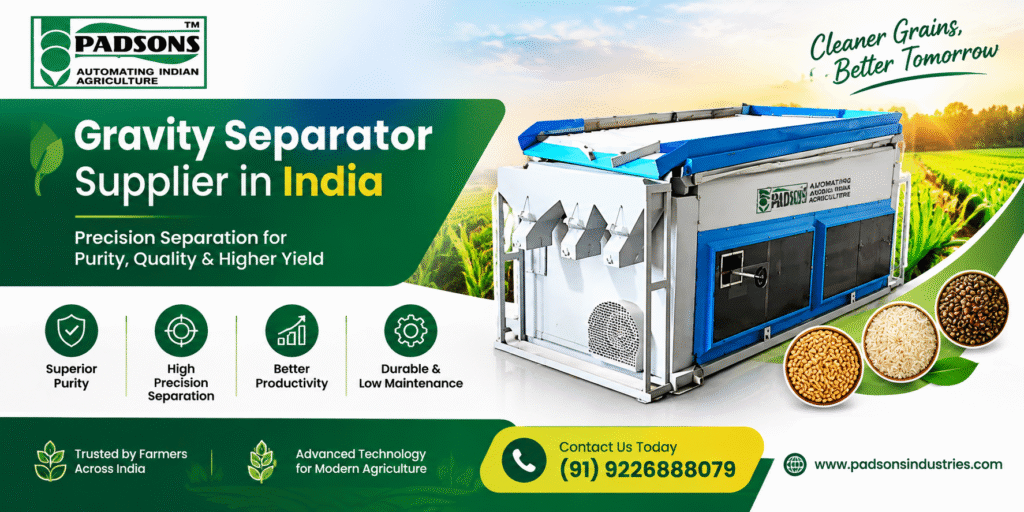
Gravity Separator Supplier in India
Introduction
At Padsons Industries, we specialise in crafting user-friendly manual and semi-automatic farm machinery. With a focus on simplicity and effectiveness, our equipment is designed to make farming tasks more efficient and accessible for all. Our range includes a variety of tools that cater to the diverse needs of farmers. From easy-to-use ploughs to hassle-free seeders, we take pride in creating machinery that simplifies the farming process. With decades of experience in the industry, we understand the challenges faced by modern-day farmers. That’s why we’re dedicated to providing practical solutions that enhance productivity and yield. Trust Padsons Industries to be your reliable partner in agriculture.
In the agriculture and food processing industry, proper cleaning and separation of grains, seeds, pulses, and other agricultural products is very important. Removing impurities and separating materials according to their physical properties helps improve product quality, reduce processing losses, and increase overall efficiency. A Gravity Separator is one of the most useful machines for achieving accurate separation.
Padsons Industries is a trusted name for industrial and agricultural processing machinery. The company focuses on providing practical and efficient equipment designed to support modern grain and seed processing operations. For businesses looking for reliable grain cleaning equipment, choosing an experienced Gravity Separator Supplier in India is important. The right supplier can provide suitable machinery, dependable performance, and solutions according to different processing requirements. We are the best Gravity Separator Manufacturer.
What Is a Gravity Separator
A gravity separator is a specialised machine used for separating grains, seeds, and other agricultural products based on their specific weight or density. It uses controlled airflow and vibration to separate heavier and lighter particles. We are the best Gravity Separator Exporter.
During the separation process, heavier and high-quality materials move in one direction while lighter and unwanted materials are separated from them. This makes the machine useful for improving the overall quality of processed products. Gravity separators are commonly used in grain processing plants, seed cleaning facilities, food processing industries, and agricultural operations.
Applications of Gravity Separators
1. Seed Processing Industry
- One of the most important applications of a gravity separator is seed processing. Seed processors need to remove immature, shrivelled, insect-damaged and low-density seeds from healthy seeds. A gravity separator helps classify seeds according to their specific gravity, allowing heavier and healthier seeds to be separated from lighter and defective seeds. This can help seed processors achieve better purity and more uniform seed lots.
2. Grain Cleaning and Grading
- The grain processing industry is another major application area. Wheat, rice, maize, barley and other grains may contain lightweight, damaged or immature kernels even after conventional cleaning. A gravity separator separates these materials according to density and helps improve the overall quality of the processed grain. This is especially useful when grains have similar dimensions but different weights.
3. Rice and Paddy Processing
- Rice mills and paddy processing plants can use gravity separation to remove low-density and defective material from the product stream. During processing, some grains may be immature, damaged or partially filled. A gravity separator can help separate these lighter particles from heavier, better-quality grains.
4. Pulses and Dal Processing
- Pulse processing is another important application for gravity separators. Pulses such as chickpeas, pigeon peas, green gram, black gram and lentils can contain broken, shrivelled, immature or lightweight particles. A gravity separator helps separate these materials from good-quality pulses. It can be used after other cleaning and grading stages to provide additional density-based separation.
5. Wheat Processing
- Wheat processing requires effective removal of inferior kernels and unwanted material before further processing. A gravity separator can be used to separate wheat grains according to density. It is particularly useful for removing shrivelled, damaged and lightweight kernels that may be difficult to separate through size-based screening alone.
6. Maize and Corn Processing
- Maize and corn processing plants can use gravity separators for density-based grading. The machine can separate heavier, better-quality kernels from lightweight, damaged or immature material. Gravity separation can be integrated with other equipment such as cleaners, graders, elevators and conveyors to create a complete processing line.
7. Oilseed Processing
- Oilseeds such as soybean, mustard, sunflower, sesame and groundnut can also be processed using gravity separation equipment. Oilseed batches may contain lightweight, immature or damaged seeds. A gravity separator can help separate these unwanted materials based on specific gravity. For oilseed processors, better separation can contribute to improved raw-material quality before further processing.
8. Groundnut and Peanut Processing
- Groundnut processing requires the separation of good-quality kernels from lightweight and defective material. Gravity separators can be used as part of groundnut cleaning and grading lines. By using airflow and vibration, the machine separates particles according to density and helps processors obtain a more uniform product. This is particularly useful for processors supplying peanuts for food processing, packaging and further manufacturing.
9. Spice Processing
- Spice processing is another application of gravity separators. Products such as coriander, cumin, pepper and other dry spices may contain lightweight particles, broken material, shells, stems or other unwanted components. A gravity separator can provide density-based separation after initial cleaning. Industry sources identify spices as one of the common product categories handled by gravity separation equipment.
10. Coffee Processing
- Coffee processing plants can use gravity separators for separating coffee beans according to density. This can help remove lighter or defective beans and improve uniformity in the processed coffee stream. Gravity separation is used in coffee dry-mill applications and can be combined with other coffee-processing machinery. For coffee processors, better density-based grading can support improved consistency in the final product.
Benefits of Gravity Separator
1. Better Separation Accuracy
- One of the main benefits of a gravity separator is its ability to separate products according to their specific gravity. Materials with different densities can be separated effectively, helping remove unwanted particles, immature grains, damaged seeds, and other impurities. A dependable Gravity Separator Supplier in India can provide equipment designed for accurate and consistent separation according to the requirements of different processing applications.
2. Improved Product Quality
- Product quality is important for manufacturers, processors, exporters, and agricultural businesses. Gravity separators help remove low-quality and unwanted materials from the final product. For example, in grain and seed processing, lighter, damaged, or poorly developed seeds can be separated from healthy and heavier seeds. This improves the overall quality and appearance of the finished product.
3. Higher Processing Efficiency
- Modern gravity separators are designed to handle continuous processing with efficient material flow. This allows businesses to process larger quantities of material in less time. By selecting the right machine from an experienced Gravity Separator Supplier in India, companies can improve their production process while maintaining consistent separation performance.
4. Reduction in Material Wastage
- Traditional manual sorting methods can result in inconsistent separation and unnecessary product loss. Gravity separators provide a controlled separation process that can help reduce wastage. The machine separates materials according to their density and other physical characteristics, allowing valuable products to be recovered more efficiently.
6. Consistent Separation Performance
- Consistency is essential in industrial processing. Manual sorting depends heavily on workers and can vary from one batch to another. A properly designed gravity separator provides controlled operating conditions, helping maintain more uniform separation results. This can be particularly useful for businesses handling large quantities of agricultural or food-processing materials.
7. Improved Seed Processing
- The agricultural and seed-processing industries can benefit significantly from gravity separation technology. Seeds that have different densities can be separated to improve the quality of the seed lot. Removing lightweight, damaged, or underdeveloped seeds can help processors obtain a more uniform and higher-quality product.
8. Labour Saving
- Manual sorting and separation can require significant manpower, especially when large quantities of material need to be processed. Gravity separators automate much of the separation process, reducing dependence on manual labour. This can help businesses use their workforce more efficiently and concentrate on other important production activities.
9. Easy Integration into Processing Lines
- Gravity separators can often be integrated with other equipment used in processing plants. They can work as part of a larger cleaning and grading system. Depending on the application, a processing line may include equipment such as cleaners, graders, elevators, conveyors, destoners, and gravity separators. A suitable Gravity Separator Supplier in India can help businesses select equipment that fits their existing processing setup.
10. Better Handling of High-Volume Production
- Industries dealing with large quantities of grains, seeds, and agricultural products need reliable processing equipment. Gravity separators are suitable for applications where continuous and efficient material separation is required. The appropriate machine capacity can be selected according to production requirements, helping businesses maintain a smooth processing operation.
11. Improved Final Product Value
- Better separation can directly contribute to better product quality. When unwanted and low-density materials are removed effectively, the final product can become more suitable for further processing, packaging, or sale. For manufacturers and exporters, consistent product quality can also help meet customer expectations and maintain long-term business relationships.
Why Choose Padsons Industries
1. High-Quality Manufacturing
- One of the main reasons to choose an Indian supplier is access to locally manufactured equipment. Established suppliers generally focus on using suitable materials, reliable components, and proper manufacturing processes to produce durable machines. A well-designed gravity separator should be capable of continuous operation while maintaining consistent separation performance. Quality manufacturing can also help reduce unnecessary breakdowns and maintenance requirements.
2. Cost-Effective Solutions
- Indian manufacturers can provide gravity separator solutions at competitive prices compared with many imported alternatives. Local manufacturing helps reduce several additional costs associated with international sourcing, including shipping, import duties, and long-distance logistics. This makes an India-based Gravity Separator Supplier a practical option for businesses looking for a balance between machine quality, performance, and investment.
3. Customised Gravity Separators
- Every processing plant may have different requirements. The type of material, production capacity, particle characteristics, available space, and desired separation efficiency can vary from one application to another. Experienced Indian suppliers can offer customised machines according to the customer’s requirements. Customisation may include machine capacity, feeding arrangements, screening systems, airflow settings, dimensions, and other application-specific features.
4. Efficient Operation
- Processing plants need machines that can operate efficiently for long periods. A well-designed gravity separator can provide continuous separation while maintaining controlled material movement. Adjustable airflow and deck settings allow operators to modify the machine according to the characteristics of the material being processed. This flexibility can be especially useful when processing different varieties of seeds or grains.
5. Better Technical Support
- Purchasing industrial equipment is not only about receiving the machine. Proper installation, operation, maintenance, and troubleshooting are also important for long-term performance. An experienced Gravity Separator Supplier in India can provide technical assistance during installation and commissioning. Suppliers with technical teams can also guide operators about machine settings, operating procedures, and routine maintenance.
6. Faster Communication and Service
- Working with a domestic supplier can make communication easier. Customers can directly discuss their requirements with the manufacturer or technical team without depending on international communication channels. Local suppliers can also respond more quickly to service requirements, spare-part inquiries, and technical questions. This can be particularly valuable for industries where production downtime can result in significant losses.
7. Availability of Spare Parts
- Regular maintenance is essential for industrial machinery. Components may eventually require replacement because of normal wear and continuous operation. Choosing an Indian supplier can make it easier to source replacement components and spare parts. Local availability can reduce waiting periods and help businesses keep their equipment operational.
8. Easy Transportation and Installation
- India has a strong manufacturing and transportation network. Suppliers can arrange transportation of industrial machinery to different parts of the country. Local sourcing can also simplify coordination related to installation, commissioning, and service visits. This can save time compared with importing equipment from overseas manufacturers.
9. Focus on Energy-Efficient Operation
- Modern industrial equipment is increasingly designed with operating efficiency in mind. A properly designed gravity separator can help businesses achieve the required separation while maintaining efficient material flow and machine operation. Energy consumption should be considered along with capacity, separation efficiency, maintenance requirements, and overall machine performance when selecting equipment.
10. Reliable After-Sales Support
- After-sales service is one of the most important factors when purchasing industrial machinery. Even a high-quality machine may require technical assistance, maintenance, adjustments, or replacement parts during its operating life. A dependable supplier should provide support after installation and help customers resolve operational issues when required.
How to Select the Right Gravity Separator
Before purchasing a gravity separator, businesses should evaluate several factors.
- Material Type: Different grains and seeds may require different machine settings and configurations.
- Required Capacity: Select equipment according to the quantity of material that needs to be processed per hour.
- Separation Requirements: Understand the quality and density differences that need to be separated.
- Machine Construction: A strong and durable construction is important for continuous industrial operation.
- Ease of Maintenance: Equipment should be convenient to inspect, clean, and maintain.
- Supplier Support: Technical assistance and after-sales support can be important for long-term machine performance.
Choosing the right Gravity Separator Supplier in India can help businesses avoid unsuitable equipment and improve their overall processing efficiency.
Conclusion
A gravity separator is an important machine for industries involved in grain, seed, pulse, and agricultural product processing. Its ability to separate materials according to density and specific gravity makes it useful for improving product quality and processing efficiency.
Padsons Industries can be regarded as a trustworthy industrial machinery provider for companies searching for durable processing equipment. Padsons Industries strives to assist clients in enhancing their manufacturing processes by emphasising quality, application needs, and useful processing solutions.
